Quick answer: Target poisoning is the progressive formation of a reacted compound on a sputtering target during reactive sputtering. As compound coverage increases, sputter yield, discharge behavior, deposition rate, and film composition can change together. The practical goal is not always to eliminate the compound layer; it is to identify a stable operating window and control it with signals that are meaningful for the specific target, reactive gas, power supply, pumping system, and film requirement.
What is target poisoning in reactive sputtering?
Reactive sputtering introduces a gas such as oxygen or nitrogen into an inert sputtering atmosphere to form a compound film. The reactive species can react at the substrate, on chamber surfaces, in the gas phase, and at the target. Target poisoning describes the condition in which a compound-rich layer develops on the target surface.
This is a surface-coverage problem rather than a simple on/off event. A target can operate with predominantly metallic surface coverage, partial compound coverage, or extensive compound coverage. The consequences depend on the target–gas pair. A compound-covered surface may have a different sputter yield and secondary-electron emission behavior from the underlying metal. If the reaction product is electrically insulating, charge accumulation and arcing can also become important.
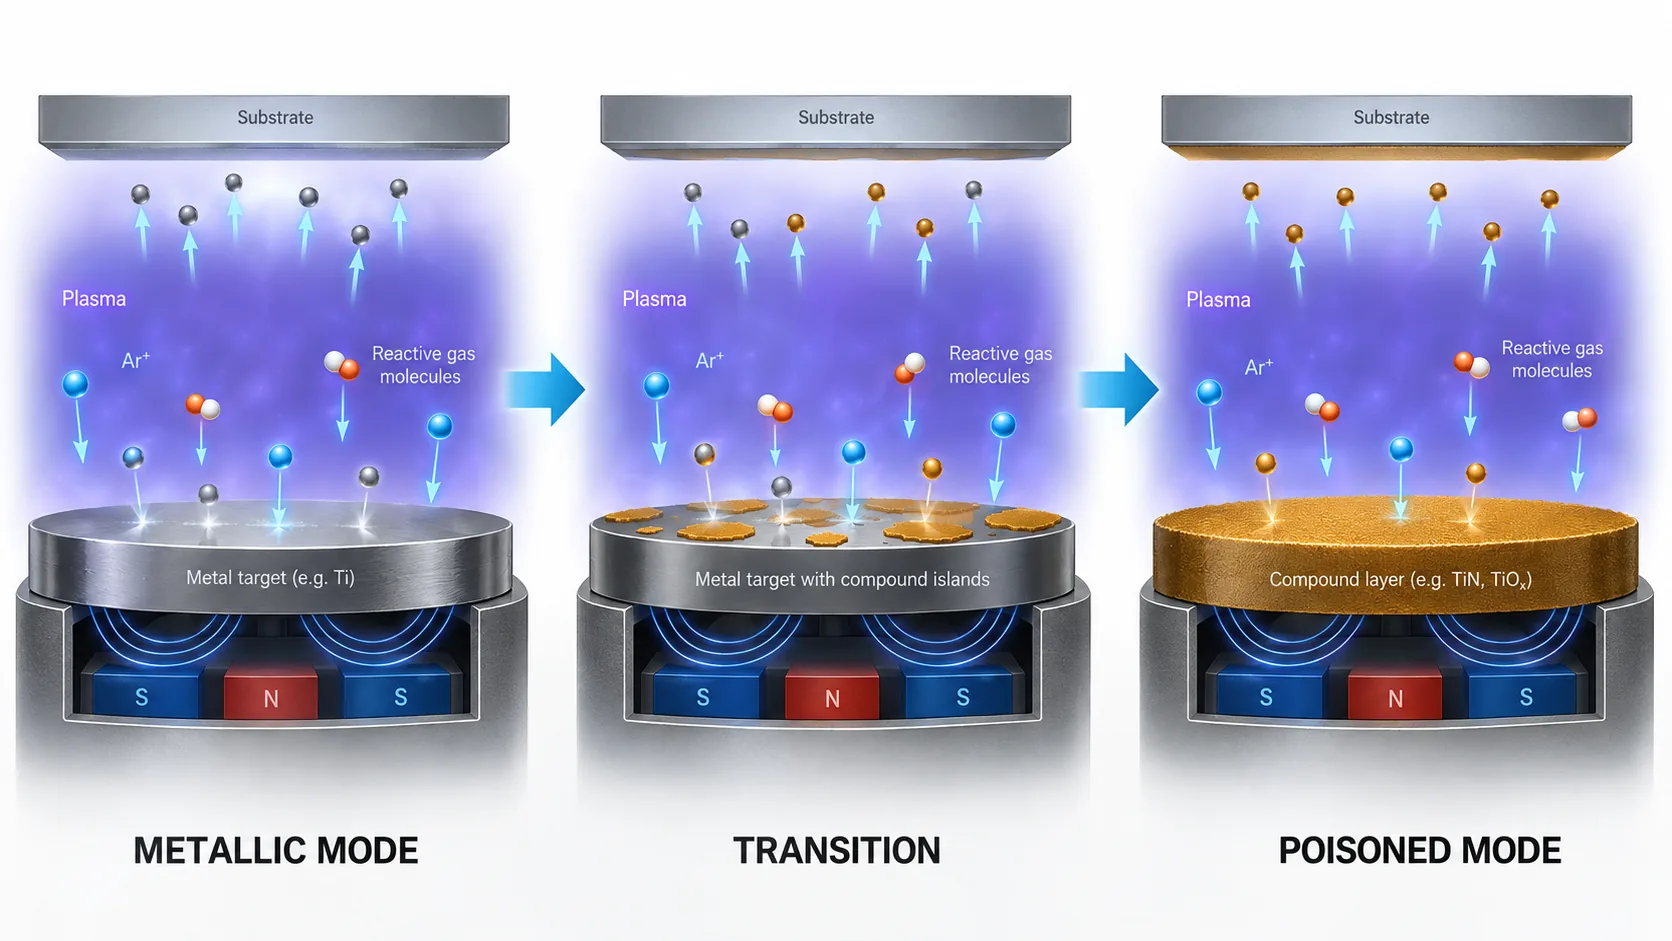
Why poisoning and hysteresis occur
The target surface is governed by competing rates. Reactive species arrive and form or implant into a compound-rich surface, while ion bombardment removes material. Chamber walls and the growing film also consume reactive gas. When metallic surfaces are available, this gettering can keep the reactive-gas partial pressure relatively low. As the available metallic surface decreases, gas consumption changes and the reactive partial pressure can rise sharply.
The classic Berg model represents this behavior with gas and material balances at the target and collecting surfaces. Later work has extended the model to account for mechanisms beyond simple chemisorption. Direct experimental analysis of Ti in Ar/N2, for example, confirmed nitrogen uptake and hysteresis and found retained nitrogen beyond a single adsorbed monolayer, consistent with implantation-related mechanisms.
Hysteresis means that the process follows different paths when reactive-gas input is increased and decreased. A flow setpoint that appears stable on the upward sweep may not represent the same target coverage on the downward sweep. This is why a single flow value, copied from another tool or process, is not a transferable recipe.
Metallic, transition, and poisoned operating modes
| Mode | Typical target condition | What may change | Control implication |
|---|---|---|---|
| Metallic mode | Target surface remains largely unreacted | Relatively high metal sputter flux; the film may be reactant-deficient if gas supply is insufficient | Useful for rate, but film composition must be verified |
| Transition region | Metallic and compound-covered areas coexist | Small disturbances can produce large changes in partial pressure, emission, voltage, rate, or composition | Often requires fast, closed-loop control |
| Poisoned mode | Compound coverage dominates the target surface | Sputter yield and electrical behavior may differ substantially; insulating coverage can promote arcing | Can be stable, but rate and power-delivery constraints must be accepted and verified |
“Poisoned” does not automatically mean that the film is defective. A compound-mode process may be selected when it offers the required stoichiometry or reproducibility. Conversely, metallic-mode operation is not automatically correct if the resulting film is under-reacted. The valid operating point is defined by film acceptance data, not by mode labels alone.
What operators can monitor
No single diagnostic is universal. Select signals that respond monotonically and repeatably in the relevant process window, and correlate them with film measurements.
- Reactive-gas partial pressure: a residual-gas analyzer or other partial-pressure sensor can indicate how much reactive gas remains after system consumption.
- Optical emission: plasma-emission monitoring can track a selected metal or gas line and drive closed-loop gas control. Published Ti–N work demonstrated stable operation using plasma-emission feedback, but its numerical setpoints are specific to that experiment.
- Discharge voltage, current, or impedance: useful trend signals in many systems, but the direction and sensitivity of the response depend on material, power mode, and operating point.
- Arc counts and power-supply events: especially relevant when insulating regions form on a DC-driven target or nearby surfaces.
- Deposition-rate monitoring: quartz-crystal monitoring or calibrated thickness measurements can reveal rate changes, provided geometry and tooling factors are controlled.
- Film measurements: composition, optical constants, resistivity, phase, or another application-specific output must close the loop between plasma signals and the product requirement.
How to diagnose an unstable process
- Freeze the configuration record. Record target material and condition, target age or erosion state, cathode and anode condition, power mode, substrate geometry, gas species and purity, flow-control hardware, pressure-control mode, pumping configuration, base pressure, and conditioning sequence.
- Run a controlled up/down sweep. Change one independent variable in small steps, allow the system to settle, and record reactive-gas input against partial pressure, optical emission, voltage/current, deposition rate, and arc events. Do not assume that the return path matches the increasing-flow path.
- Separate electrical instability from composition drift. Arcing, a rate change, and off-stoichiometric films can occur together, but they are not interchangeable measurements.
- Inspect gas delivery and pumping. Flow-controller response, throttle behavior, conductance, leaks, outgassing, and gas-inlet distribution can move or broaden the transition.
- Verify the film. Select a proposed operating window only after the relevant film property has been measured across repeat runs.
Mitigation and control options
Closed-loop reactive-gas control
Feedback control adjusts reactive-gas delivery from a measured partial-pressure or optical-emission signal. Classic work showed that closed-loop mass-flow control could operate near the knee of a hysteresis curve without allowing the target to become fully poisoned. The controller bandwidth, sensor delay, chamber volume, pumping speed, and gas-distribution response all affect whether this approach remains stable.
Pulsed DC, bipolar, or RF power
Power-mode changes can help manage charge accumulation and arcing when insulating films form. They do not remove the underlying surface-reaction balance. A stable discharge still needs an operating window that produces the required film composition and rate.
Pumping speed, pressure, and reactive-gas distribution
Modeling and experiments show that target size, pumping speed, total pressure, gas mixture, and target composition can affect hysteresis. Changing one of these may shift or reduce the unstable region, but the result must be mapped on the actual chamber. Gas-ring or inlet placement can also create local differences that a single chamber sensor does not reveal.
Conditioning and repeatable starting state
A documented pre-sputter and gas-introduction sequence helps establish a repeatable surface state. The sequence should define shutters, power ramp, pressure stabilization, gas order, and the criterion for beginning deposition. Cleaning or conditioning advice must be compatible with the actual target, bond, backing plate, cathode, and chamber procedure.
Common troubleshooting mistakes
- Treating plasma color as a calibrated endpoint. A visual color change can be a clue, but optical-emission control uses selected spectral signals and calibration.
- Assuming discharge voltage always changes in one direction. Voltage response can be non-monotonic and material-dependent.
- Copying a gas-flow number from another chamber. Flow alone omits pumping speed, conductance, target area, wall condition, pressure, and sensor location.
- Assuming RF eliminates poisoning. RF can sustain a discharge with insulating material, but compound coverage can still change sputter yield, rate, and composition.
- Changing target design before proving the cause. First distinguish target-surface chemistry from cooling, mounting, bond, gas delivery, power-supply, and chamber-condition problems.
Target and RFQ information that matters
If process development points to a target-related constraint, send enough information for engineering review. TFM’s sputtering target catalog covers the main target families, while ceramic sputtering targets and target bonding and backing-plate services provide more specific selection paths.
- Target material, nominal composition, and required impurity or analysis limits
- Planar or rotary geometry, dimensions, tolerances, and drawing revision
- Bonded or unbonded configuration, backing-plate material, and cathode interface
- Power mode and intended power-density range, stated by the buyer rather than inferred
- Reactive and inert gases, pressure-control method, cooling arrangement, and conditioning sequence
- Observed symptoms, time-stamped trend data, arc logs, target photographs, and erosion history
- Film composition or functional acceptance criterion and the measurement method
Evidence boundary: TFM can review target form, dimensions, composition request, bonding, and supplied process context. A material quote is not a guarantee of a deposition recipe or film result. Final process-window validation remains specific to the buyer’s equipment, film stack, and acceptance method unless a documented development scope states otherwise.
Send your target drawing and process symptoms for engineering review.
References
- S. Berg and T. Nyberg, “Fundamental understanding and modeling of reactive sputtering processes,” Thin Solid Films 476 (2005) 215–230. https://doi.org/10.1016/j.tsf.2004.10.051
- W. D. Sproul, P. J. Rudnik, C. A. Gogol and R. A. Mueller, “High rate reactive sputtering process control,” Surface and Coatings Technology 33 (1987) 73–81. https://doi.org/10.1016/0257-8972(87)90178-2
- D. Güttler et al., “Mechanisms of target poisoning during magnetron sputtering as investigated by real-time in situ analysis and collisional computer simulation,” Applied Physics Letters 85 (2004). https://doi.org/10.1063/1.1835002
- S. Inoue et al., “Dynamic Process Control of rf Reactive Sputtering by Monitoring Plasma Emission Intensity,” Journal of the Japan Institute of Metals 61 (1997) 1108–1114. https://doi.org/10.2320/jinstmet1952.61.10_1108
- S. Berg et al., “Applying ‘the upgraded Berg model’ to predict hysteresis free reactive sputtering,” Surface and Coatings Technology 279 (2015) 39–43. https://doi.org/10.1016/j.surfcoat.2015.07.054