Backing plate selection affects heat transfer, thermal expansion, mechanical support, assembly weight and cathode compatibility. This guide compares common materials and explains how to screen a bonded sputtering target assembly before technical review.
Quick Answer / Selection Summary
Select the backing plate by the dominant assembly requirement, not by thermal conductivity alone. OFHC copper is a common starting point when cooling, machinability and bonding compatibility are priorities. Consider molybdenum when expansion control is critical, aluminum when weight is the constraint, and titanium when corrosion compatibility matters. Copper alloys, stainless steel or composite structures address specific mechanical or combined requirements.
Final selection must account for the target material and dimensions, bonding method, CTE mismatch, thermal management, cathode interface, cooling conditions, plate stiffness and mechanical requirements. A highly conductive plate cannot compensate for poor bonding, rear contact or cooling.
Quick Selection Table
| Material | Consider When | Main Limitation |
|---|---|---|
| OFHC Copper | Cooling and machinability are priorities | Higher CTE and weight |
| Molybdenum | Low expansion and dimensional stability are critical | Cost, density, and machining difficulty |
| Aluminum | Large assemblies require weight reduction | High CTE and surface preparation requirements |
| Titanium | Corrosion resistance or environmental compatibility is required | Low thermal conductivity |
| Copper Alloy | Higher strength, thread durability, or handling resistance is needed | Lower conductivity than OFHC copper |
| Stainless Steel | Threads, retainers, fixtures, or structural features are required | Poor primary heat spreading |
| Composite Structure | One metal cannot balance all required properties | Additional interfaces and manufacturing complexity |
This table supports initial screening. It does not define guaranteed specifications or operating limits. Verify the selected grade, product condition, temperature-dependent properties and assembly requirements before design approval.
Why the Backing Plate Matters and How to Select It
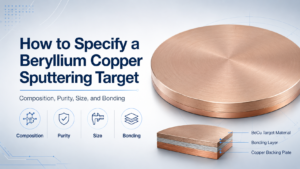
A bonded sputtering target assembly normally contains three functional components:
- The target supplies the material deposited as a thin film.
- The bonding layer joins the target to its support.
- The backing plate supports the target and transfers heat toward the cathode.
During operation, heat follows a continuous path:
Target → Bonding Layer → Backing Plate → Cathode → Cooling Water
A weakness anywhere along this path can increase the target temperature.
Even a highly conductive backing plate cannot compensate for large bonding voids, excessive bond-line thickness, poor rear-surface contact, inadequate cooling-water flow, or a warped cathode.
Similarly, a compliant bonding layer cannot fully protect a brittle target when the target and backing plate expand at substantially different rates.
A backing plate must therefore perform four connected functions:
- Remove heat from the target
- Provide mechanical support
- Control thermal expansion and distortion
- Remain compatible with the bonding method and cathode
These functions should not be evaluated separately. Improving one property may weaken another.
For example, molybdenum provides lower thermal expansion than copper but is more expensive and difficult to machine. Aluminum reduces weight but has a higher coefficient of thermal expansion. Titanium resists corrosion but transfers heat much less effectively than copper.
The best material is therefore the one that addresses the dominant constraint of the assembly.
What Each Backing Plate Material Does
OFHC Copper: The Standard Starting Point
Oxygen-free high-conductivity copper is widely used because it provides an effective balance of thermal conductivity, machinability, and bonding compatibility.
It can be machined with:
- Holes and threads
- Steps and recesses
- Grooves and cooling features
- Chamfers
- Locating features
- Cathode-specific rear geometries
OFHC copper backing plates are commonly used for circular, rectangular, stepped, segmented, and bonded target assemblies.
Copper is usually appropriate when:
- Cooling is the primary requirement.
- Target dimensions are moderate.
- Cooling is distributed uniformly.
- Assembly weight is acceptable.
- The CTE difference is manageable.
- Plate thickness provides sufficient rigidity.
This makes copper particularly useful behind brittle ceramic targets, oxide targets, semiconductor targets, and thin metallic targets requiring mechanical reinforcement.
Its main limitations are weight, softness, and relatively high thermal expansion.
For large targets, full copper backing plates can become heavy. Thin copper features may also deform under clamping or repeated installation. For low-CTE target materials, copper expansion may contribute to bowing or edge stress.
Copper can be a useful starting point, but it is not an automatic final choice.
Molybdenum: Controlling Expansion and Distortion
Molybdenum is considered when dimensional stability is more important than maximum thermal conductivity.
Its low coefficient of thermal expansion can reduce differential movement between the backing plate and low-CTE target materials.
For free expansion, the dimensional change is proportional to plate length, CTE and temperature rise. A bonded assembly is constrained, so a free-expansion calculation does not predict its deformation or interfacial stress.
Molybdenum may be suitable for:
- Large low-CTE targets
- Precision semiconductor applications
- Brittle materials sensitive to edge stress
- Repeated thermal cycling
- Assemblies in which copper produces unacceptable bowing
Its disadvantages include high density, high cost, and difficult machining.
Molybdenum should therefore solve a specific expansion or dimensional-stability problem. It should not be treated as a general upgrade from copper.
Aluminum: Reducing Assembly Weight
Aluminum is mainly considered when the mass of a full copper backing plate becomes a practical limitation.
This may occur in large-area display, photovoltaic, architectural coating, or other systems where source weight affects handling, mounting, or equipment loading.
Aluminum offers useful thermal conductivity at much lower density than copper. However, the design must also account for:
- Higher thermal expansion
- A stable surface oxide
- Lower high-temperature strength
- Surface preparation before bonding
- Cooling-water compatibility
- Galvanic interaction with other metals
- Required plate stiffness
Aluminum is therefore a weight-saving solution rather than a direct thermal equivalent to copper.
It is most appropriate when reduced mass is a defined requirement and its higher CTE can be managed through geometry, bonding design, or a composite structure.
Titanium: Improving Corrosion Resistance
Titanium may be considered when cooling-water chemistry, process conditions, or surrounding equipment makes copper less suitable.
It provides good corrosion resistance, moderate thermal expansion, and lower density than copper or molybdenum.
Its principal limitation is low thermal conductivity.
Titanium is generally better suited to specialized or low-to-moderate heat-load assemblies than to the main heat-spreading plate behind a high-power target.
Where both corrosion resistance and heat transfer are required, titanium may be more suitable as one functional part of the assembly rather than as the complete backing plate.
Copper Alloys: Adding Mechanical Strength
Pure copper may deform under high clamping loads or repeated installation.
A specified copper alloy can provide:
- Higher strength
- Better thread durability
- Greater resistance to handling distortion
- Improved stability around thin machined features
The trade-off is normally lower thermal conductivity than OFHC copper.
Copper alloys are therefore useful when mechanical durability becomes more important than achieving the highest possible conductivity.
The exact alloy grade should be specified because its strength, conductivity, corrosion resistance, and machinability can vary significantly.
Stainless Steel: Supporting Structural Features
Stainless steel is generally better suited to structural parts than to the main cooling plate.
Typical uses include:
- Threaded sections
- Retaining rings
- Clamps
- Fixtures
- Structural frames
- Reinforcing features
Its relatively low thermal conductivity makes it unsuitable for primary heat spreading in most high-power target assemblies.
The exact stainless steel grade should also be specified because ferritic and austenitic grades differ in conductivity, thermal expansion, magnetic behavior, and corrosion resistance.
Composite Backing Plates: Combining Different Functions
A composite backing plate becomes reasonable when no single metal can satisfy the critical requirements at the same time.
A one-piece copper plate remains preferable when it already provides:
- Adequate cooling
- Manageable expansion
- Sufficient rigidity
- Acceptable weight
- Reliable bonding compatibility
A solid plate has fewer interfaces, simpler manufacturing, and fewer potential failure locations.
Composite structures become useful when different layers must perform different functions.
Cu-Mo and Cu-W Structures
Cu-Mo and Cu-W combine copper’s heat-transfer and bonding characteristics with the lower thermal expansion or greater stiffness of molybdenum or tungsten.
They may be considered for:
- Low-CTE target materials
- Precision semiconductor assemblies
- Large targets sensitive to bowing
- Brittle targets exposed to thermal cycling
- Designs in which solid copper creates excessive expansion
The layer thickness, joining method, machining sequence, and residual stress must be controlled carefully.
A poorly designed composite may add thermal resistance and manufacturing complexity without providing sufficient benefit.
Cu/Al/Cu Structures
A Cu/Al/Cu structure uses an aluminum core to reduce weight while retaining copper surfaces for target bonding and cathode contact.
Its reliability depends on:
- Layer thickness
- Joining method
- Interface flatness
- Residual stress
- Machining sequence
- Cooling design
- Thermal cycling resistance
In specialized designs, different layers may be assigned to target bonding, expansion control, weight reduction, cathode contact, corrosion resistance, or structural reinforcement.
However, every added interface can introduce:
- Thermal contact resistance
- Residual joining stress
- Distortion
- Flatness variation
- Machining difficulty
- Delamination risk
A composite structure should therefore be selected only when its functional benefit clearly outweighs the added complexity.
Bonding Compatibility, Failure Analysis, and Technical Review
Backing Plate and Bonding Compatibility
Backing plate material cannot be evaluated separately from the bonding system.
Indium bonding is often used for brittle ceramic, oxide, and semiconductor targets because it provides thermal contact while accommodating limited differential movement.
Elastomeric or epoxy-based bonding systems may be selected for other target materials, operating temperatures, or stress-control requirements.
Important bonding variables include:
- Bond-line thickness
- Bond coverage
- Void control
- Surface cleanliness
- Wetting quality
- Flatness
- Operating temperature
- Thermal cycling frequency
- Target brittleness
- Backing plate expansion
The target-side surface may require controlled roughness, plating, grooves, a machined recess, or defined edge clearance.
The rear surface must maintain uniform contact with the cathode.
A compliant bonding layer can reduce stress, but it cannot correct an unsuitable backing plate material, insufficient thickness, poor flatness, or incompatible geometry.
What Backing Plate Failures Can Indicate
Backing plate-related problems commonly appear as cracking, hot spots, bowing, corrosion, or repeated debonding.
| Observed Problem | Factors to Investigate |
| Edge cracking | CTE mismatch, edge constraint, uneven bond thickness, or excessive thermal cycling |
| Local hot spots | Bond voids, poor rear contact, insufficient cooling flow, or surface distortion |
| Assembly bowing | Plate stiffness, residual machining stress, CTE mismatch, or non-uniform bonding |
| Repeated debonding | Surface preparation, wetting, bond temperature limit, or thermal overload |
| Rear-surface corrosion | Cooling-water chemistry, galvanic interaction, or incompatible materials |
These symptoms should be evaluated together with:
- Target quality
- Bond condition
- Cathode flatness
- Cooling performance
- Rear-surface contact
- Sputtering power
- Operating cycle
- Installation and clamping conditions
A target crack does not automatically prove that the target material was defective. Likewise, repeated debonding does not always indicate that the bonding material was unsuitable.
Failure analysis should consider the complete assembly.
Information Needed for Technical Review
A technical review is more reliable when the backing plate, bonding method, cathode, and operating conditions are considered together.
| Information | Details to Provide |
| Target | Material, composition, purity, density, and dimensions |
| Backing plate | Material preference, dimensions, thickness, recesses, holes, and threads |
| Cathode | Source model, assembly drawing, or interface dimensions |
| Bonding | Indium, elastomer, epoxy, customer-specified method, or unbonded |
| Operating conditions | Sputtering mode, power, cooling arrangement, and operating cycle |
| Quality requirements | Tolerances, inspection reports, material certificates, quantity, and documentation |
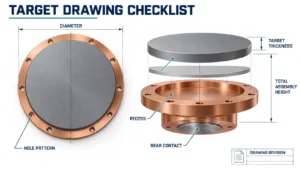
A drawing is preferable to a photograph for replacement assemblies.
Photographs may show the general configuration, but they cannot reliably confirm:
- Flatness
- Parallelism
- Thickness
- Recess depth
- Hole position
- Thread specification
- Rear contact geometry
- Dimensional tolerances
For an OEM replacement, the preferred reference is the original engineering drawing, assembly drawing, cathode interface drawing, or an inspected sample component.
Backing Plate Reuse, Replacement, and OEM Reproduction
A used backing plate can often be reused, but reuse should be based on inspection rather than appearance alone. After debonding and cleaning, the plate should still meet the dimensional, mechanical, and interface requirements of the sputtering source.
When Can a Backing Plate Be Reused?
Reuse may be possible when the backing plate remains flat, sufficiently thick, free from serious corrosion, and compatible with the new target and cathode. Hole positions, threads, recess depth, rear contact surfaces, and cooling features must also remain within acceptable condition.
What Should Be Inspected Before Reuse?
The following items should be checked:
- Flatness and parallelism
- Remaining thickness
- Recess depth
- Corrosion or oxidation
- Hole and thread condition
- Overheating marks
- Residual indium or adhesive
- Rear contact surface
- Cooling channels or interfaces
- Compatibility with the new target
Cleaning or light machining may be required before rebonding.
When Should the Backing Plate Be Replaced?
Replacement is recommended when the plate is warped, excessively corroded, overheated, too thin after cleaning, or has damaged holes, threads, sealing surfaces, or cooling features. A new plate may also be necessary when the original design no longer matches the target dimensions, installed height, or cathode interface.
Can an OEM Backing Plate Be Reproduced?
An OEM backing plate can be reproduced when its critical dimensions and interface features can be verified. A dimensioned drawing is preferred, but a physical sample may also be used for measurement and review.
Important features include:
- Overall diameter and thickness
- Recess diameter and depth
- Hole pattern and PCD
- Thread size and position
- Grooves and sealing surfaces
- Installed height
- Rear contact geometry
- Cooling features
Photos are useful for initial identification, but they are normally not sufficient for production because they cannot confirm tolerances or hidden dimensions.
Information Needed for Technical Review
For reuse or reproduction, provide the backing plate material, drawing or sample, target dimensions, cathode model, installed height, operating conditions, and any required inspection records. TFM can then review whether the plate should be reused, re-machined, or replaced.
Conclusion
OFHC copper is a common starting point for bonded sputtering targets because it offers an effective balance of cooling, machinability, and bonding compatibility.
Alternative materials should be selected only when another constraint becomes dominant.
Molybdenum can help control thermal expansion and distortion. Aluminum can reduce the weight of large assemblies. Titanium may improve corrosion resistance. Copper alloys and stainless steel can strengthen structural features.
Composite structures are appropriate when no single material can provide the required thermal, mechanical, dimensional, and weight performance.
Their value comes from purposeful layer design and reliable interfaces—not from complexity alone.
For drawing-based target assemblies, TFM can review the proposed backing plate material, geometry, bonding method, cathode interface, and possible reuse of an existing backing plate before quotation.
Technical Review and Next Steps
For project-specific bonding, backing plate machining or reuse review, see Sputtering Target Bonding & Backing Plate Services. Review the available Indium Target Bonding Service and Elastomeric Target Bonding Service with the intended target and operating conditions.
Use the Sputtering Target Drawing Checklist for RFQs to prepare interface dimensions and drawing information. Browse the Sputtering Targets hub for target materials.